
 中文(中国)


CNC machining can use the same digital model to make one prototype or a continuing production run, but the manufacturing plan changes as volume rises. A prototype program is built to learn quickly: confirm geometry, test fit, and expose design problems. Production work must repeat an approved result at a predictable rate and cost. That shift affects programming, workholding, tool management, inspection, and supplier selection. Buyers who understand those changes can compare quotations more accurately and avoid treating a successful prototype as automatic proof of production readiness.
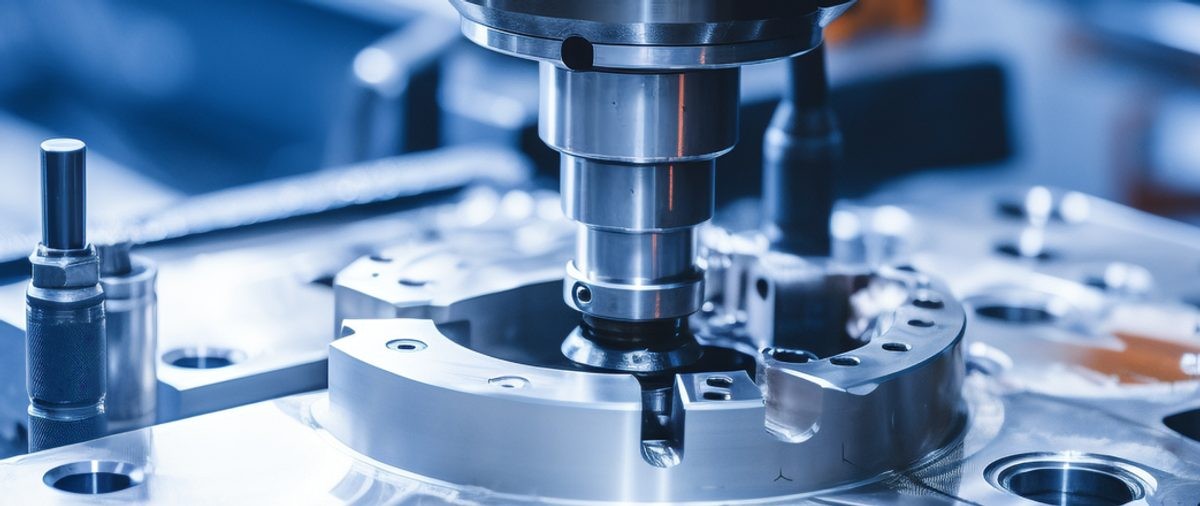
What Changes Between a CNC Prototype and a Production Run?
Prototype Work Prioritizes Speed and Learning
Prototype machining begins with uncertainty. Engineers may still be checking wall thickness, tool access, or assembly fit. Therefore, the shop needs a flexible program and practical workholding that can produce a testable part without excessive dedicated tooling. Inspection and assembly tests may trigger changes to the CAD model, datum scheme, material, or machining sequence. Before the design stabilizes, a fast feedback cycle matters more than the lowest possible unit price.
Production Work Prioritizes Repeatability and Throughput
Once the drawing and material are approved, the goal changes from exploration to controlled repetition. The manufacturer documents the process, fixes the workpiece location, standardizes tools and cutting data, and defines checks for critical features. A batch also needs predictable cycles, planned tool changes, and clear handling between roughing, finishing, deburring, treatment, and inspection. The cutting principle remains familiar, but operating discipline becomes stricter.
How CNC Machining Costs Shift as Volume Increases
Programming, Setup, and Fixturing Are Front-Loaded
Before cutting begins, the supplier reviews the drawing, selects equipment and tools, prepares the sequence and program, sets up workholding, and verifies the first acceptable part. Those activities may be necessary for one component or hundreds. Higher volume spreads the preparation across more saleable parts, although revisions and additional setups can introduce new engineering work. Dedicated fixtures add initial cost but can improve loading speed and positioning consistency. Buyers should ask how fixture cost is charged and whether the fixture can support repeat orders.
Cycle Time, Tool Life, and Yield Drive Unit Economics
After setup is distributed, recurring costs become more visible. Machine time depends on toolpaths, operations, material machinability, finish, and stock removal. Complex access can require repositioning, while tight features can need slower passes. Tools also wear, so a production quotation must allow for replacement, offsets, scrap, and rework. The best volume quotation is not simply the lowest cycle-time estimate; the quotation should reflect a stable process capable of delivering acceptable parts.
Why Process Control Gets Stricter at Production Volume
Tolerances Move from Single-Part Proof to Repeatable Capability
Order volume does not change the drawing tolerance. Volume changes the evidence needed to show that the process can hold that tolerance repeatedly.
Production must manage variation from tool wear, heat, clamping, stock condition, and machine behavior. Excessive clamping can distort a thin part, while weak clamping can allow movement. Separating rough and finish operations may also help manage heat and residual stress before final dimensions are produced.
Inspection Plans Expand Beyond a Final Check
A scaled order needs checks at the points where problems can still be contained. Incoming inspection can confirm material identity and condition. First-part verification checks the setup before the batch proceeds. In-process measurements can reveal drift early enough to adjust an offset or replace a tool. Final inspection confirms that completed parts meet the agreed requirements.
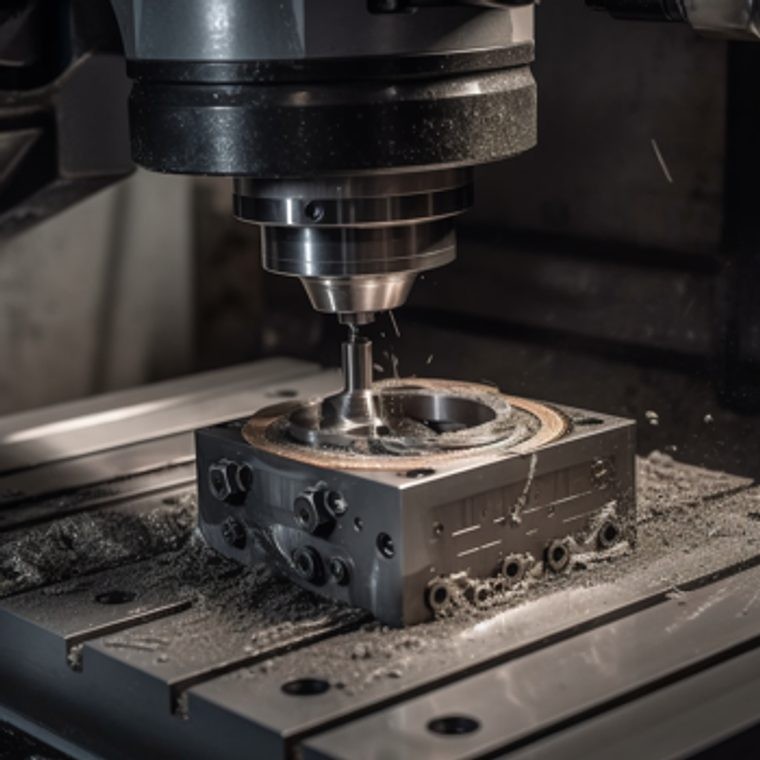
Not every feature needs the same frequency or equipment. Critical dimensions, fit relationships, safety-related characteristics, and hard-to-rework features deserve more attention than noncritical surfaces. Buyers should agree on the inspection plan, reporting format, sampling method, and response to a nonconforming result before production starts.
When Should Buyers Change the Manufacturing Plan?
Choose Fixtures and Automation Around Stable Demand
Investment becomes easier to justify when the design, material, and forecast are stable. Dedicated fixtures, preset tools, probing, or automated loading can reduce handling and variation, but each option adds engineering effort and may reduce flexibility. The decision depends on expected demand, repeat frequency, labor, setup time, and quality risk. A reusable fixture or proven program may create value across the product lifecycle.
Compare CNC with Another Process Before Scaling Further
CNC remains useful when material properties, tight features, or revisions make hard tooling unattractive. With stable demand, another process may offer better economics: injection molding can suit repeat plastic parts, while additive manufacturing may fit complex low-volume geometry. No universal break-even quantity applies. Size, material, tooling complexity, finish, tolerance, forecast certainty, and revision risk all affect the comparison.
How Momaking Supports CNC Projects from One Part to Batch Production
Quote and Process Review Before Cutting Starts
At Momaking, we support rapid prototyping and batch production through an online CNC workflow. Buyers can upload a 3D file, then align material, process, quantity, and finishing requirements. Our public service information presents a one-piece minimum, quotations generated in seconds, and delivery as fast as two days for suitable jobs. Actual timing and cost depend on the design. We can also review whether difficult features create extra operations or another manufacturing route deserves comparison.
Machining, Materials, and Inspection in One Workflow
Our documented capabilities include CNC multi-axis options, turning, milling, and drilling. The published range covers aluminum, stainless, and alloy steels, copper alloys, engineering plastics, and selected special materials. We also state that parts receive full inspection before delivery. Buyers should still identify critical dimensions, required reports, finishes, and application-specific acceptance rules so our team can build the quotation and inspection approach around the real commercial risk.
FAQ
Q: Is CNC machining economical for low-volume production?
A: It can be. CNC avoids the dedicated mold required by some processes, but programming and setup still influence the first units. Geometry, material, tolerance, and revision risk determine the result.
Q: Why does CNC unit cost often fall as volume increases?
A: Programming, setup, and fixture work can be distributed across more acceptable parts. Savings may be offset by extra tooling, inspection, handling, or capacity requirements.
Q: Do CNC machining tolerances change with order volume?
A: The drawing tolerance stays the same. Higher volume requires stronger evidence that workholding, tools, temperature, and inspection can maintain the requirement throughout the run.
Q: When should a buyer switch from CNC machining to another process?
A: Compare processes when demand becomes stable enough to justify dedicated tooling or when geometry favors another method. Use lifecycle volume, quality risk, revision probability, material, and total cost rather than a universal quantity threshold.